Sheet metal
Parts in as fast as 5 days. Laser cutting, CNC punching, and brake forming in steel, stainless, and aluminum, domestic and overseas.
Engineer reviewed quote
Want to learn more? Read on.
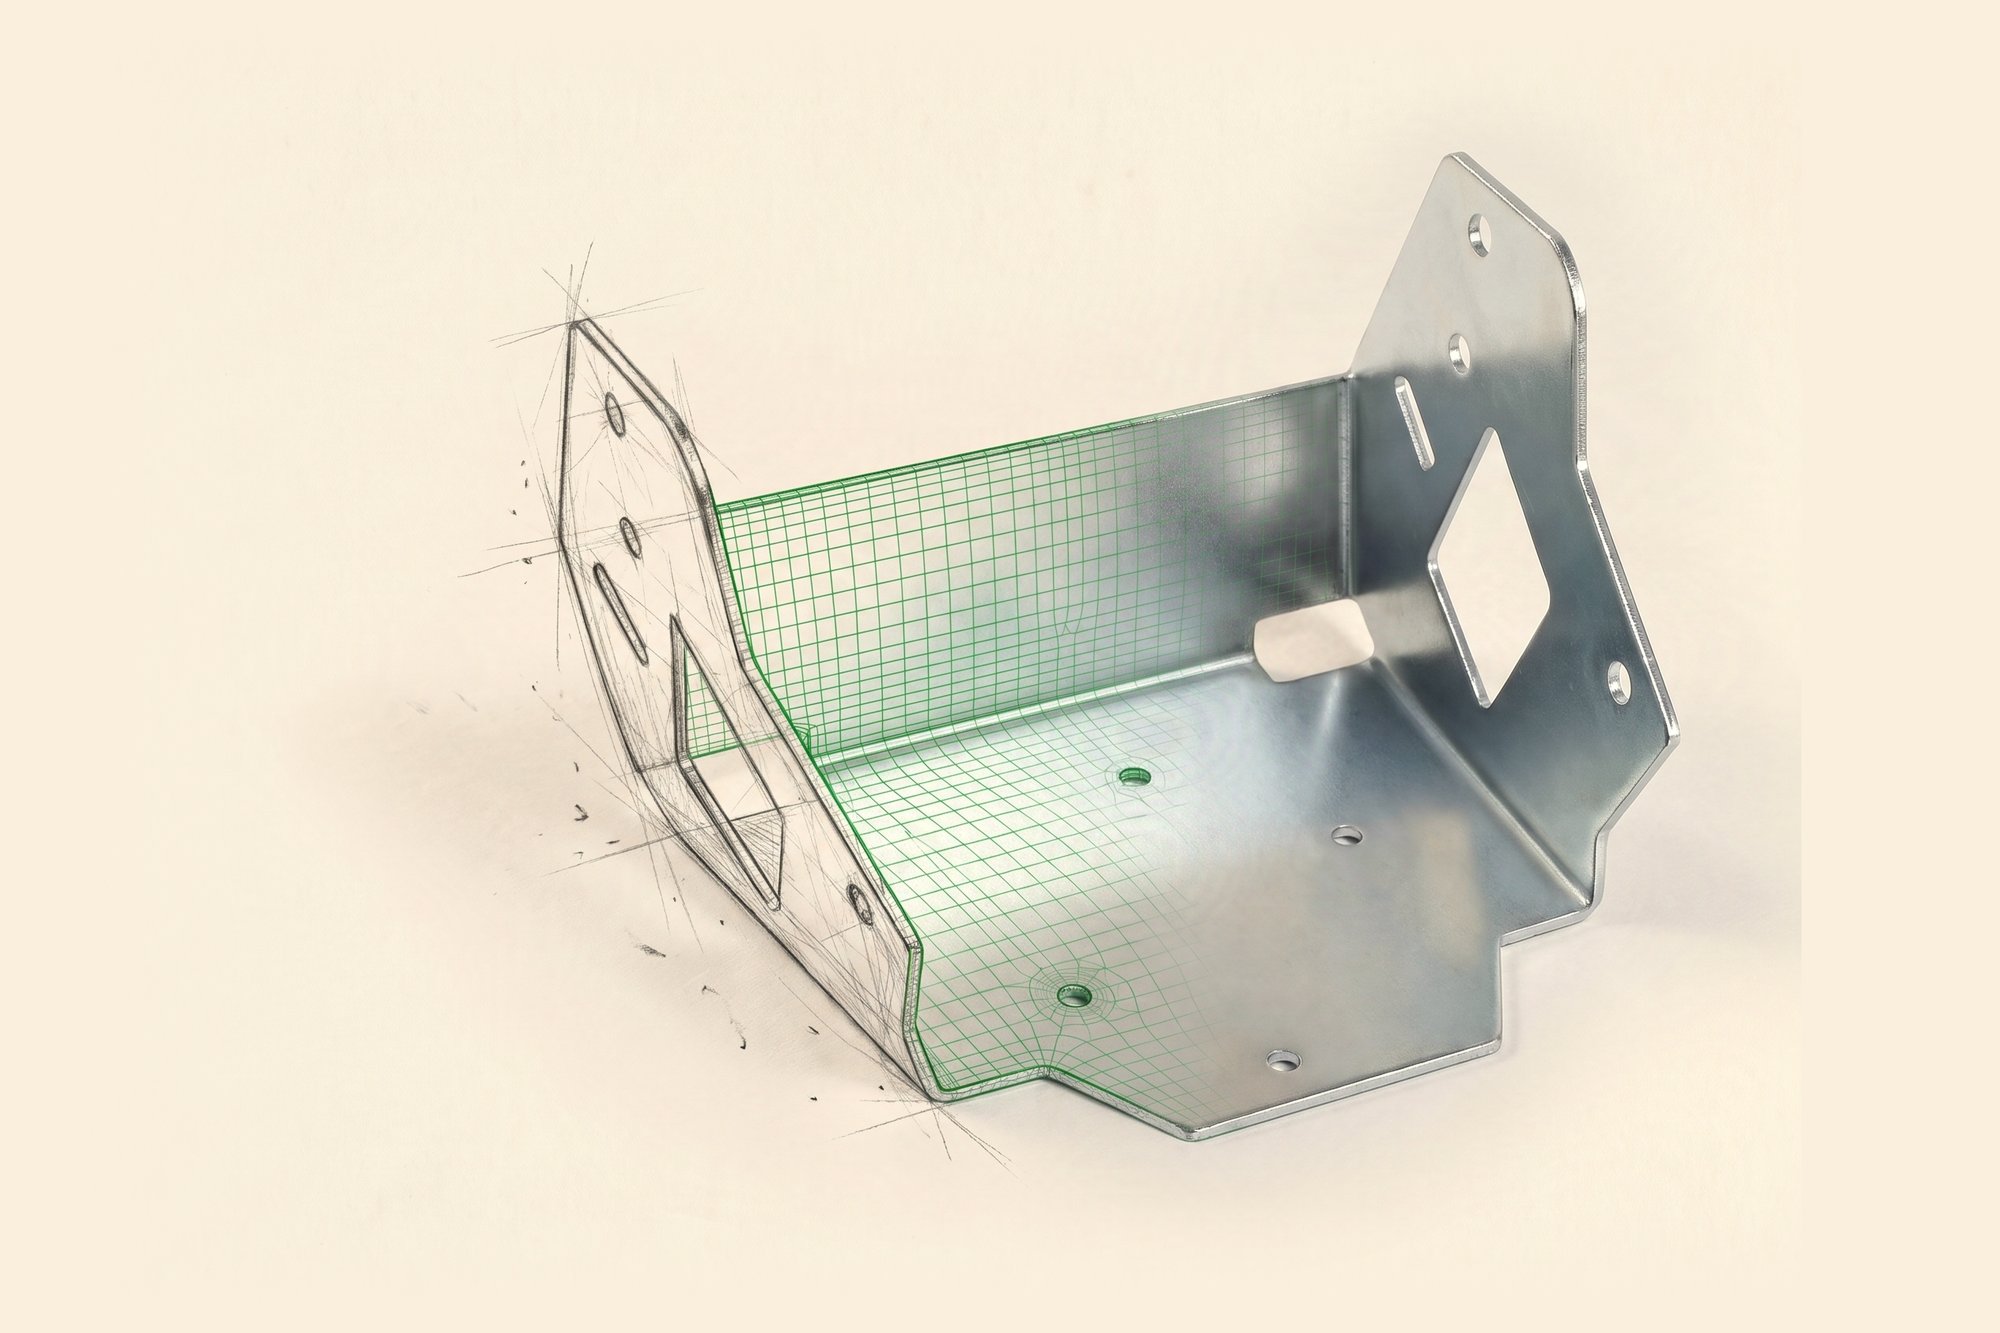
Formed parts we ship.
Laser cut, punched and brake formed in steel, stainless and aluminum. Every quote starts from the flat pattern.
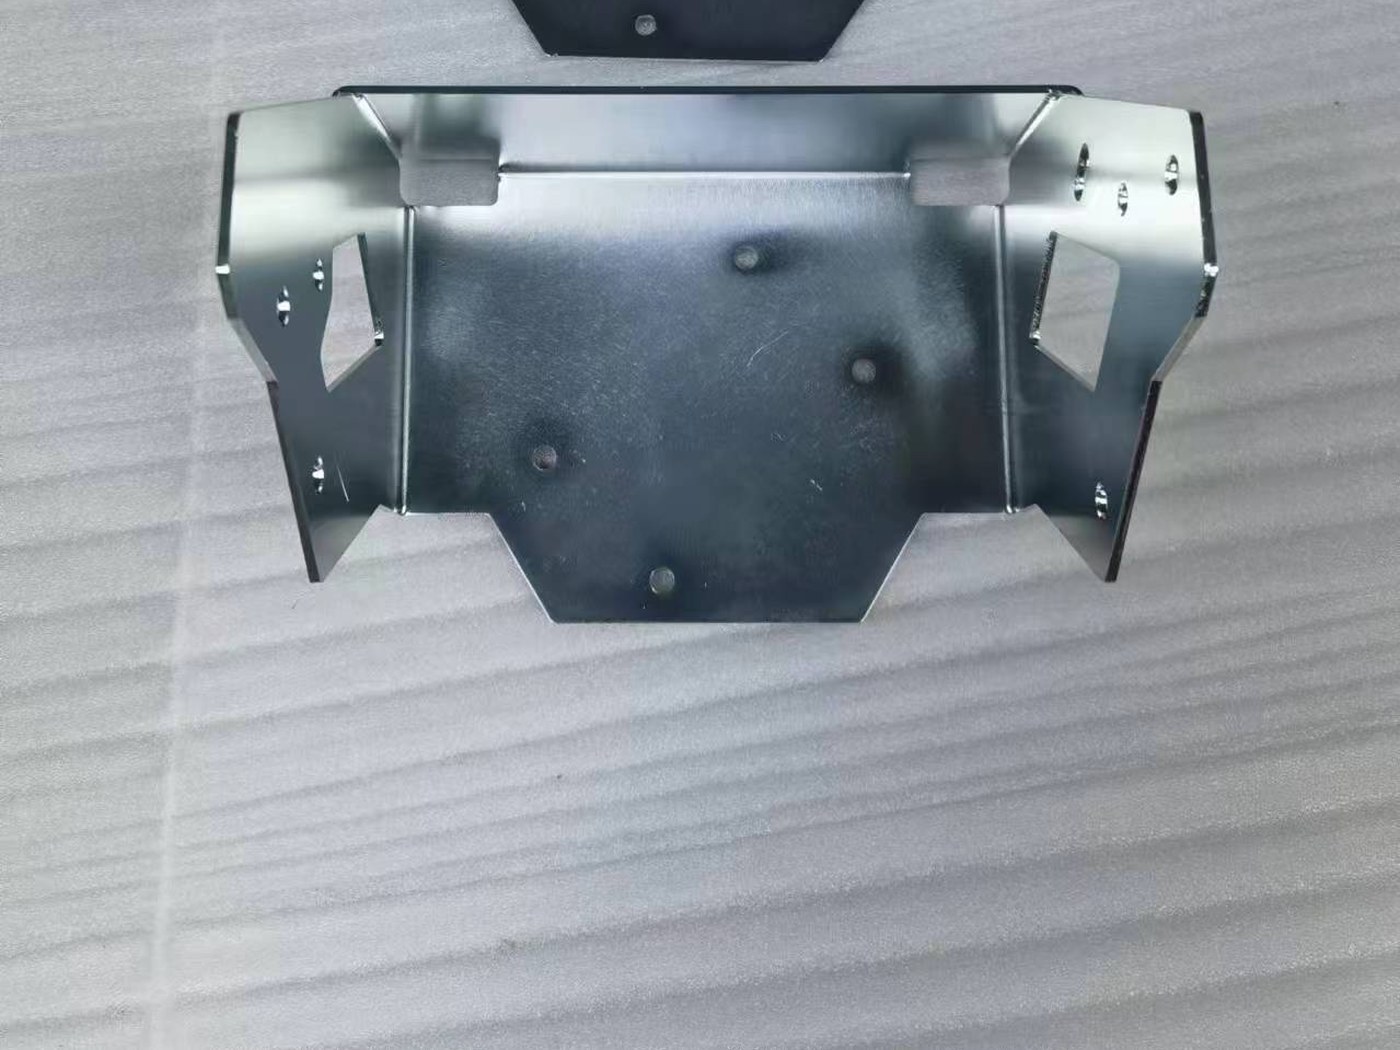
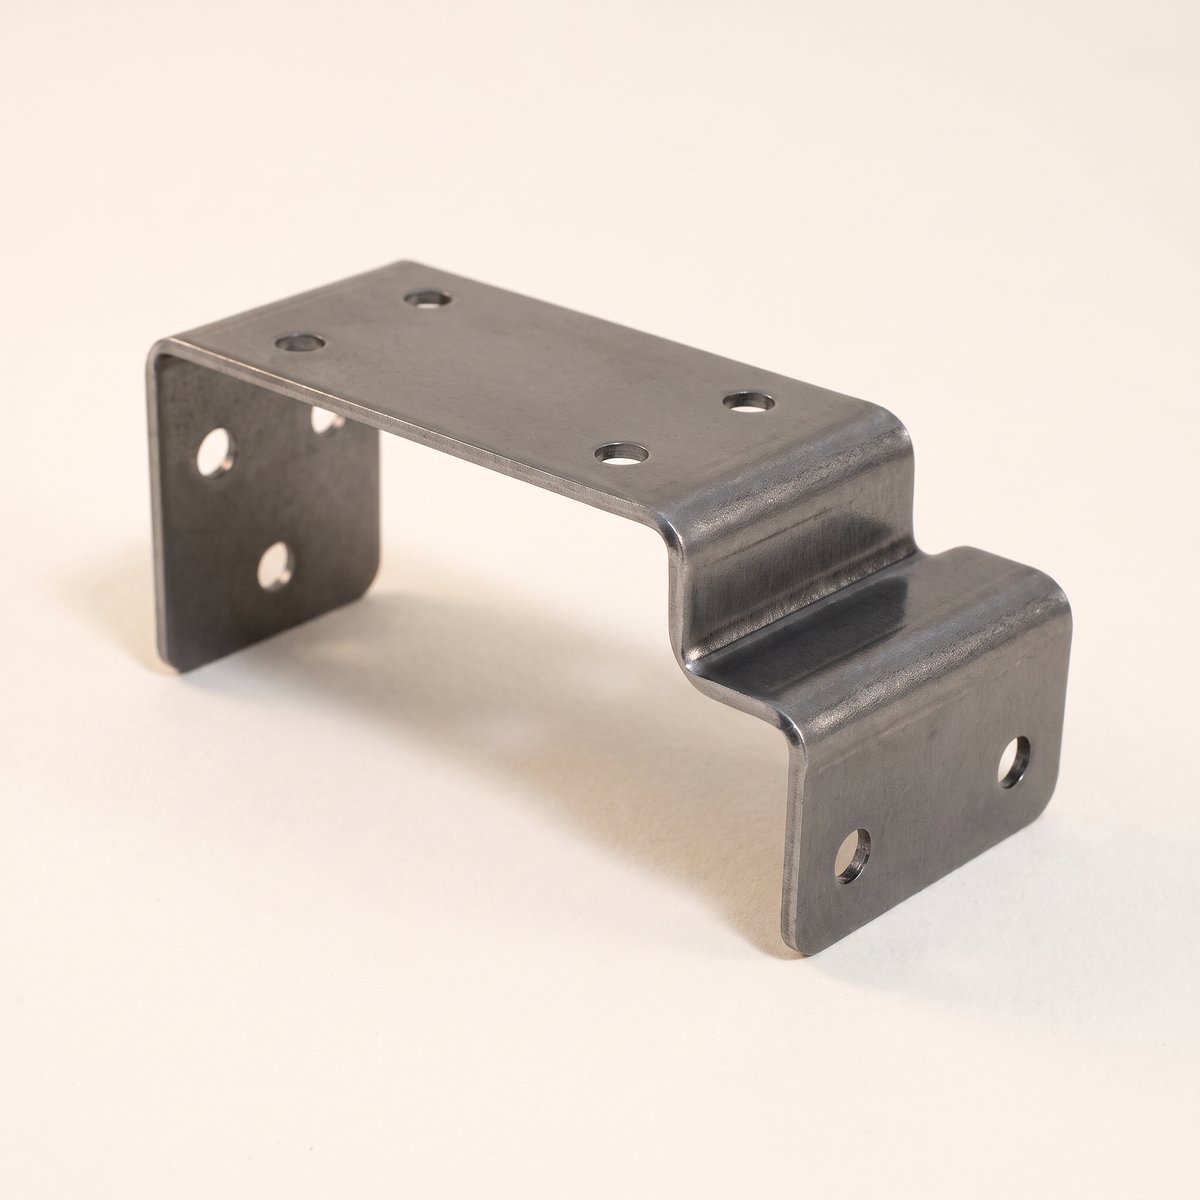
Formed bracket
Laser cut blanks with the flanges brake formed and the slots punched in.
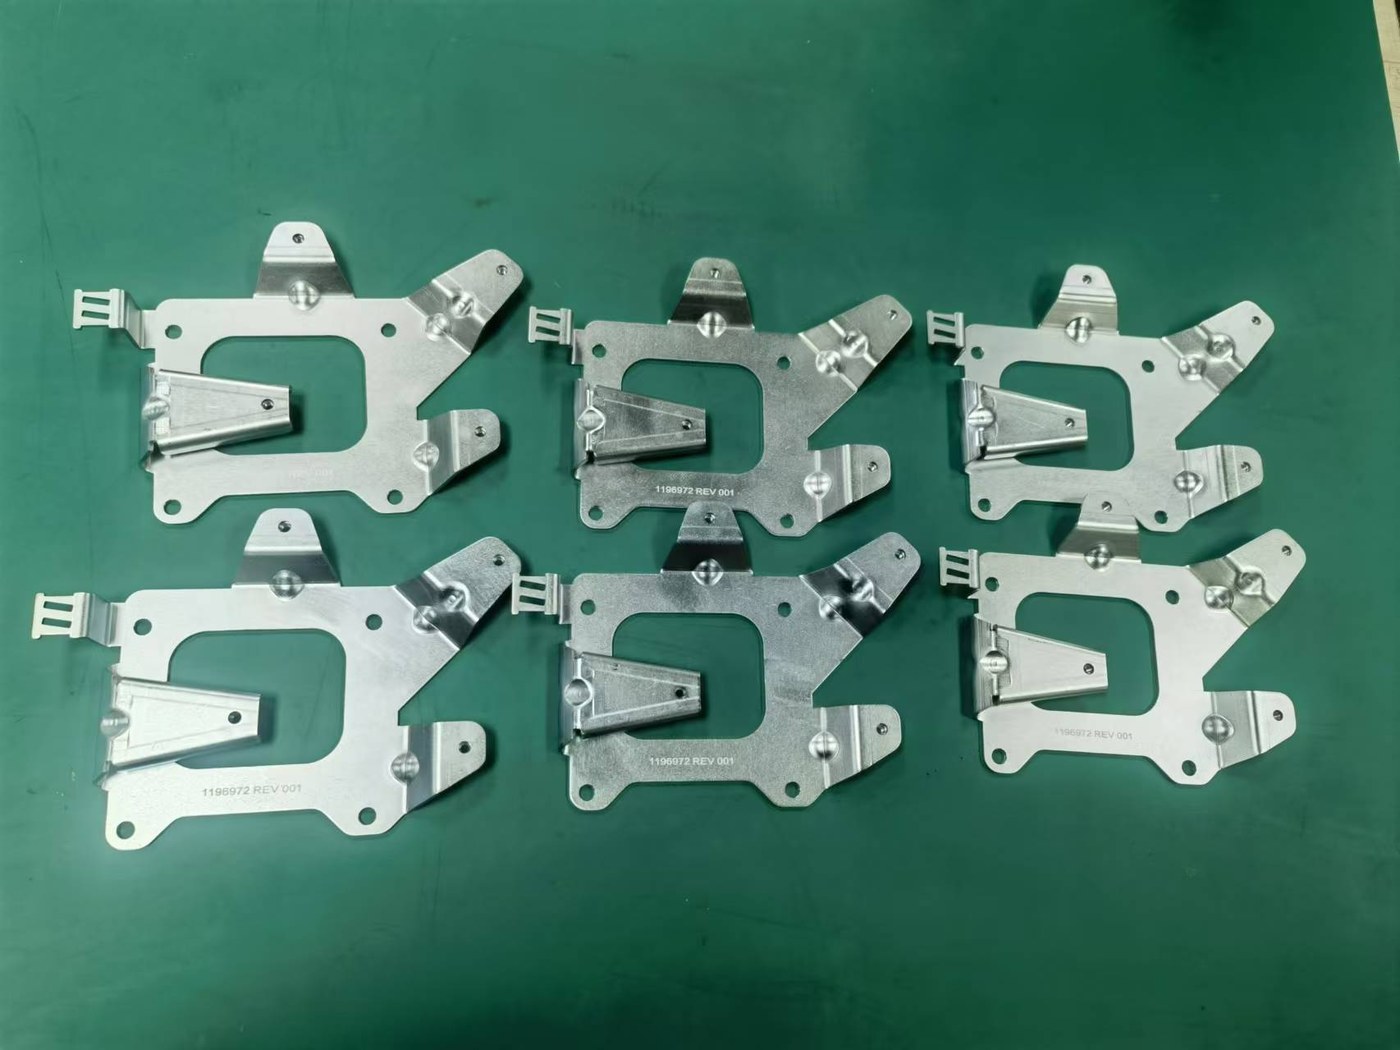
Plated bracket batch
Formed, zinc plated and run as a batch to one print.
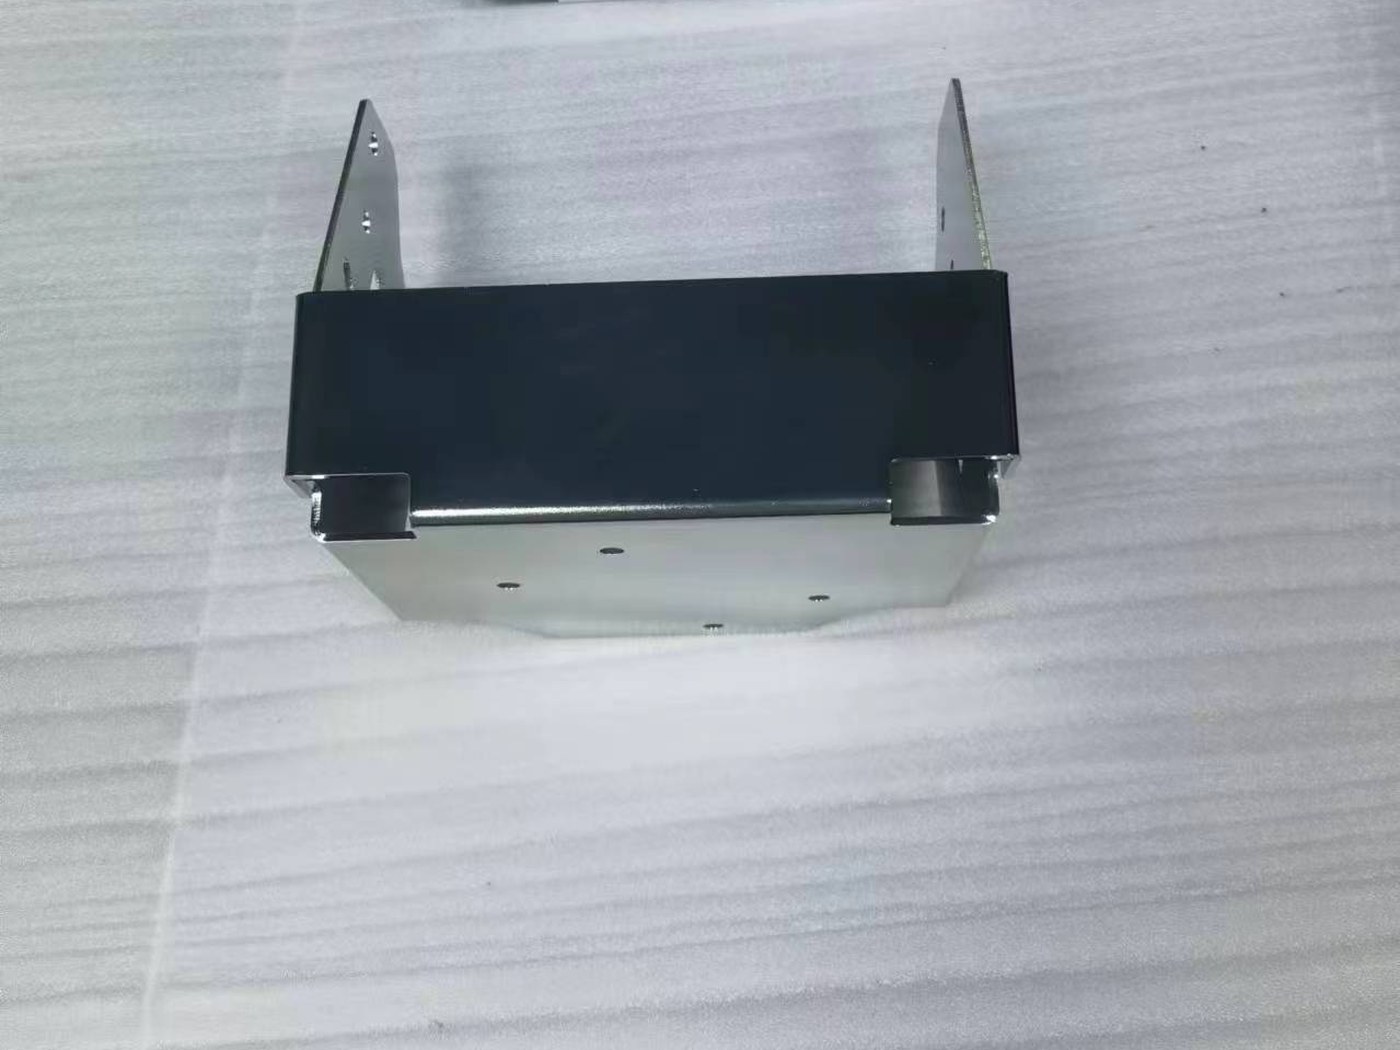
Formed enclosure
Multi bend box formed on the brake from a single blank.
Design guidance
8-point design checklist
Design to these eight points and your part quotes faster and forms cleaner. Bend geometry, hole placement, and hardware fit are where most sheet metal parts get expensive.
Bend radius
Inside radius held to at least material thickness so bends form without cracking or thinning.
Bend relief
Relief cuts added at flange edges so the brake doesn't tear or distort the adjacent material.
Hole-to-bend distance
Holes kept clear of the bend zone, minimum 2.5x thickness plus radius, so they don't deform when formed.
Hole-to-edge distance
Edge margins set to at least 2x thickness so holes stay round and edges stay flat.
Minimum flange length
Flanges kept long enough to seat in the brake, roughly 4x thickness plus radius.
K-factor & bend allowance
Flat pattern developed from the actual K-factor for the material and tooling so formed dimensions land on print.
Material & thickness
Gauge and alloy matched to strength, corrosion, and forming needs before the flat is cut.
Hardware & inserts
PEM nuts, standoffs, and studs specced for the gauge so pull-out and torque targets hold.
Processes
Fabrication processes
Most parts touch two or three of these before they ship. We route the whole part through one shop so the cut, the form, and the finish all answer to the same traveler.
Laser cutting
Fiber lasers cut clean flat blanks from thin gauge up to plate. Tight kerf, no tooling cost, quick turns on revisions.
Punching & stamping
CNC turret punching for high-volume flats and repeat features. Hard tooling for stamped brackets when the volume justifies it.
Brake forming
Press brakes form flanges, hems, and complex multi-bend parts. Flat patterns developed from the real K-factor so bends land on print.
Welding & hardware
TIG, MIG, and spot welding for weldments and enclosures. PEM nuts, standoffs, and studs pressed in for fastening that holds.
Sheet metal materials
The alloy sets the strength, the corrosion behavior and how the part forms before the first bend. Pick a family to see what it holds, how it bends and what to watch for. Bring the environment and the load case and we will land on the gauge and grade.
Cold rolled steel (1008 / 1010)
Formability
Excellent
Tensile strength
~45,000 psi
Corrosion resistance
Low, needs a finish
Weldability
Excellent
Density
7.85 g/cm³
Cost
$
Common gauges
24 ga to 7 ga (0.024" to 0.179")
Typical uses
Brackets, enclosures, chassis, weldments
Watch for
Every cut edge rusts, so the finish is part of the print. Call out powder coat, plating or e coat and the masking that goes with it.
Finishes
Powder coat, zinc plate, e coat, wet paint
Finishing
Coatings and finishes
Finish is part of the quote, not an afterthought. We handle it in-network so the part ships ready to install.
Powder coat & wet paint
Durable color and corrosion protection in a full RAL range, with masking for grounds and threads.
Plating & passivation
Zinc, nickel, chromate, and stainless passivation for corrosion and conductivity.
Anodizing
Type II and hardcoat on aluminum for wear resistance and cosmetic color.
Silk screen & overlays
Legends, logos, and graphic overlays applied to panels and faceplates.
Deburr & finish
Edge break, graining, and bead blast so parts are safe to handle and ready to coat.
Materials, tolerances, finishes.
No minimum. We cut single prototypes through production runs of tens of thousands. Setup and programming cost comes down per-part on larger batches and repeat orders.
Cold rolled and hot rolled steel, stainless 304 and 316, aluminum 5052 and 6061, galvanized steel, copper, brass, and spring steel. Gauges from 0.020" up to 0.250". Material sourced to ASTM specs with certs on request.
Tolerances are set per feature at quote, with the tooling and fixturing chosen to hold the critical dimensions. Flat patterns are developed from the actual K-factor so formed dimensions land on print.
Fiber laser cutting, CNC turret punching, press brake forming, stamping, hardware insertion (PEM), TIG and MIG welding, spot welding, and deburring. Multiple processes on one part are routed through a single traveler.
Powder coating, wet paint, anodizing, chromate/passivation, zinc and nickel plating, silk screen, and graphic overlays. Finish and masking requirements are reviewed during DFM.
STEP (.stp) and SolidWorks native for 3D, DXF for flat patterns, and 2D drawings in PDF for tolerances, bend, hardware, and finish callouts. STEP is preferred; a flat DXF speeds up quoting.
As fast as 5 days for straightforward brackets and panels in common gauges. Standard is 7 to 12 business days depending on forming complexity, hardware, finishing, and quantity. Expedited options available.
ISO 9001 and ISO 13485 certified. CMM and first-article inspection available. FAI reports, material certs, and certificates of conformance provided on request.
Next step
Let's move your part forward.
Send the CAD. An engineer replies in 1 to 2 business days.
Get a Quote